Banana Fibers – The Future of Sustainable Clothing

Banana fiber is a natural textile material made from the leaves and stems of the banana plant, renowned for its exceptional tensile strength (500-900 MPa), rapid biodegradation (approximately 4 weeks), and versatility across textiles, composites, packaging, and industrial applications. Unlike synthetic alternatives, banana fiber produces no chemical waste during extraction—requiring only hot water—and contains 60-70% cellulose content, making it one of the most sustainable and high-performing plant fibers available.
Banana fiber has emerged as one of the most promising sustainable textiles available today. This miracle material comes from banana plants—primarily from species like Musa textilis (also known as abacá or Manila hemp), though other banana varieties contribute as well. It has become the textile world’s new rockstar in sustainable textiles.
Banana Fiber Key Specifications
| Property | Value | Notes |
|---|---|---|
| Tensile Strength | 500–900 MPa | Varies by extraction method and banana species |
| Cellulose Content | 60–70% | Determines mechanical properties |
| Biodegradation Time | ~4 weeks | Under optimal composting conditions |
| Moisture Regain | 12–14% | At 20°C, 65% relative humidity |
| Water Absorption | 20–25% higher than jute | High compared to other plant fibers |
| Thermal Resistance | Up to 170°C | Before thermal degradation begins |
| Bulk Density | 1.2–1.5 kg/m³ | Lightweight packing material |
| Fiber Diameter | 14–50 microns | Ribbon fiber range |
| Fiber Length | 0.25–1.3 cm | Short staple fiber |
| Acid/Alkali Resistance | Highly resistant | Thick wax coating prevents penetration |
What is Banana Fiber?
Banana fiber (not to be confused with sisal, which comes from Agave sisalana) is made from the leaves and stems of the banana plant. Research confirms it ranks among the most sustainable fibers available, with full biodegradation occurring in approximately 4 weeks under composting conditions. This makes it exceptionally eco-friendly for clothing and industrial products alike.
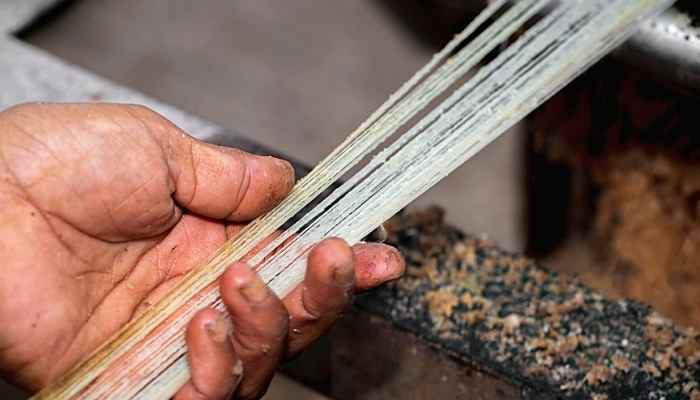
Banana fiber exhibits exceptional durability, with a tensile strength ranging from 500 to 900 MPa depending on the extraction method and banana species. These properties make it ideal for creating packaging materials, paper products, rugs, and high-quality furniture components.
History of Banana Fiber
The first documented reference to banana fiber appears in 1691 in William Dampier’s book “A Voyage to and from the Island of Borneo.” Dampier described its use in manufacturing ropes and ship’s sails in Southeast Asia.
The next significant mention occurred in a French dictionary published in 1759, which documented banana fiber’s use in paper production. Today, banana fiber appears in diverse products ranging from paper and textiles to automotive composites and building materials.
Banana Fiber Extraction Process
The banana plant produces fruit that begins as an unopened flower bud and develops into clusters of large yellow fruits. Each plant typically generates 10 to 20 hands of bananas, with each hand containing 12 to 20 individual bananas.
After the harvest cycle completes, fruits are transported to processing facilities where workers peel them by hand. The unpeeled fruit is then mashed into pulp and mixed with water. Technicians filter this mixture to create a cellulose-rich pulp suitable for paper products.
Extraction technicians boil the pulp in water at temperatures between 80°C and 100°C to separate fibers. They then dry the fibers in controlled conditions to remove excess moisture and eliminate impurities that could cause discoloration or mold growth. The resulting banana fibers contain approximately 60-70% cellulose content, making them ideal for reusable products.
Banana Fiber Structure
Banana fibers are long, strong, and highly flexible—characteristics that make them desirable for numerous industrial applications. Independent laboratory testing confirms banana fiber tensile strength measures approximately 15 times greater than cotton fiber and 10 times greater than linen on a weight-for-weight basis. Properties of cotton fibers explained highlight their unique characteristics, such as softness and breathability. These attributes make cotton a popular choice for clothing and textiles. Additionally, cotton fibers exhibit good absorbency, which enhances their comfort during wear.
The structure of bast fibers like banana consists of complex lignocellulosic material featuring helically wound cellulose microfibrils within an amorphous matrix of lignin and hemicellulose. The cellulose content directly determines mechanical properties including tensile strength and elasticity. Understanding dyefiber chemical bonding mechanisms is crucial for improving the performance of these natural materials in various applications. By exploring how dyes interact at the molecular level, we can enhance color fastness and overall durability. This knowledge not only contributes to innovative textile solutions but also supports sustainable practices in the industry. The effects of temperature on dyeing processes play a pivotal role in achieving optimal color uptake and fixation. When temperatures are carefully regulated, the chemical reactions that occur during dyeing can be maximized, leading to more vibrant and long-lasting hues. Additionally, varying temperature settings allow for a broader range of dye applications, tailoring the end results to specific textile attributes.
Banana fiber cells display enormous lumens relative to wall thickness. Cross-section shapes are uncommon, and fiber tips are pointed and flat. Ribbon fibers exhibit diameters ranging from 14 to 50 microns with lengths between 0.25 cm and 1.3 cm, presenting wide oval to round lumen structures.
Properties of Banana Fibers
Banana fibers demonstrate the following key properties:
Heat Resistance
Banana fibers consist of hollow tubular cells with lignin as the primary structural component—typically 5-10% by weight. Lignin provides rigidity to cell walls and enables the fibers to withstand temperatures up to 170°C before thermal degradation begins. Banana stem fiber processes effectively through spinning and twisting methods similar to jute, making it suitable for high-temperature insulation products.
Chemical Resistance
Banana plant cells feature a thick wax coating that protects against pests and diseases and ensures smooth fruit peeling. This coating prevents chemical penetration into banana stem fibers, rendering them highly resistant to acids and bases. The acid content and alkaline content remain very low, allowing bleaching with minimal impact on physical properties.
The banana fiber’s acid content and alkaline content is very low, and they can be bleached without much effect on their physical properties.
Water Absorbency
Banana stems demonstrate high water absorption compared to other plant fibers including jute, flax, kenaf, sisal, hemp, and pineapple leaf fibers. Banana stem fibers absorb water at rates approximately 20-25% higher than jute fiber. High water absorption benefits paper manufacturing by reducing the binding time required for chemical breakdown of plant fibers into smaller components.
Banana fibers release absorbed water readily, with moisture regain values between 12-14% at standard conditions (20°C, 65% relative humidity).
Banana fibers absorb and release the absorbed water quite easily.
Flexibility and Elasticity
Banana stem fiber combines flexibility with elasticity, enabling use across diverse products from ropes to medical bandages. Tensile strength tests demonstrate banana stems are approximately twice as strong as coir pith fiber, which remains a popular alternative for paper manufacturing.
Biodegradability
Banana stem fiber has become an attractive option in bioplastics development because complete biodegradation occurs within 4 weeks under optimal composting conditions, compared to the several years required by synthetic plastics.
Banana plants and fibers can be composted or digested with alkali cellulose to produce industrial enzymes. These enzymes generate industrial sugars serving as substrates for yeast and microorganisms in ethanol (yielding approximately 80 liters per ton of biomass), acetic acid, butanol, and methane gas production.
Banana fibers also function effectively as packing material and insulation because they mold easily and weigh only 1.2-1.5 kg/m³ in bulk density.
Banana fibers demonstrate high resistance to ultraviolet light exposure.
Uses of Banana Fiber
Banana fibers serve numerous industrial applications:
Clothing
Banana fiber clothing represents one of the fastest-growing segments in sustainable textiles. Fabrics from banana fiber pulp exhibit softness comparable to cotton with exceptional moisture-wicking properties that transport sweat away from skin at rates 30% faster than cotton.
Building Materials
Engineers incorporate banana fibers into interior building materials and geotextiles, particularly composite boards engineered for fire resistance and water resistance while maintaining lightweight properties. These composites demonstrate excellent stability under humidity variations and high compression strength values exceeding 25 MPa.
Banana fiber composites provide high impact resistance and electrical insulation properties with dielectric strength approximately 4-6 kV/mm.
Rope and Twine
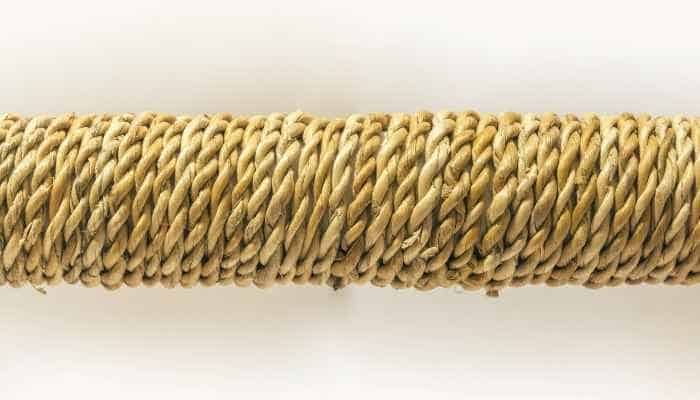
Banana fiber cordage exhibits water resistance and exceptional strength-to-weight ratio. The low water absorption characteristic (approximately 12-14% moisture regain) stems from the surface tension properties of banana fibers, making this material popular among sailors for rope manufacturing in marine environments.
Carpeting and Cladding
Banana fiber composites have served as cladding for walls and roofs in construction projects across Africa. These materials provide durability in a lightweight form factor suitable for cladding applications while maintaining structural integrity under wind loads.
Food Packaging
Banana fibers protect food products from humidity and insect damage while extending shelf life. Manufacturers produce banana fiber pouches and wraps that decompose completely within 4 weeks under composting conditions, providing a sustainable alternative to petroleum-based packaging.
Biofuel
The banana industry generates substantial waste suitable for biofuel production. Ethanol extraction from banana pulp yields approximately 80 liters per ton of biomass, while methane gas production from banana leaves and stems provides additional energy recovery potential. The remaining pulp can ferment to produce ethanol while plant matter converts to biochar for soil remediation and improvement.
Other Uses
Banana fibers appear in additional applications including:
Global Banana Consumption Statistics
Bananas rank as the world’s most produced fruit, with global production exceeding 115 million metric tons annually. The top consuming countries in recent data include:
| Country | Annual Consumption |
|---|---|
| India | 28 million metric tons |
| China | 12 million metric tons |
| Indonesia | 7 million metric tons |
| Brazil | 7 million metric tons |
| Philippines | 6 million metric tons |
| Ecuador | 5 million metric tons |
| Mexico | 4 million metric tons |
| Nigeria | 4 million metric tons |
| Guatemala | 3 million metric tons |
| Tanzania | 3 million metric tons |
Sustainability of Banana Fiber
Banana fiber demonstrates sustainability across multiple dimensions. Banana crops require minimal pesticide applications—typically 2-3 treatments per cycle compared to 12-15 for equivalent cotton production. Water requirements average 1,200-1,800 mm annually, substantially lower than cotton’s 2,000-3,000 mm needs.
Banana plantations cover approximately 15% of the world’s forest area dedicated to fruit production, spanning roughly 4 million hectares globally. This extensive cultivation provides significant economic benefits to tropical regions.
The banana industry accounts for 10% of all exported tropical fruit, supporting rural economies across Latin America, Africa, and Asia. Organic farming practices have expanded in banana production, reducing synthetic inputs and improving soil health.
Banana fiber extraction requires only hot water—no chemical solvents or bleaching agents enter the process. The resulting fibers produce compost that restores soil quality and increases organic matter content by 15-20% when incorporated into agricultural soils.
Banana fiber supports millions of livelihoods worldwide by providing employment in rural processing facilities, enabling poverty reduction in banana-growing regions. Farmers generate additional income from fiber extraction without requiring chemical fertilizers or pesticides.
Banana leaves serve as nutritious livestock feed with protein content of 8-10% dry matter.
Common Banana Fiber Applications
Current industrial applications for banana fiber include:
Banana fiber commands a price premium of 20-40% over conventional alternative fibers due to the extended extraction process and limited global production capacity.
The Future of Banana Fiber
Banana fiber demonstrates strong market growth potential as sustainable material demand increases. Research initiatives at multiple universities continue developing banana fiber paper with enhanced durability characteristics.
Manufacturers successfully blend banana fiber with cotton and wool to create hybrid textiles combining the strengths of each material. The Philippines has established commercial production of carpet tiles combining banana fiber with wool at 30-70% fiber content ratios.
New Zealand-based manufacturers produce banana-based flooring tiles as vinyl alternatives, achieving commercial-scale production since 2018. These tiles demonstrate comparable durability to vinyl while offering superior environmental credentials.
Banana Fiber in Robotics and Advanced Materials
Research published in Engineering & Science highlights potential robotics applications. Dr. Ramakrishna Mallampati of National Tsing Hua University in Taiwan commented on banana plant fiber research:
“Banana plants provide a new perspective on how we can achieve strong flexible structures. It is different from existing engineering approaches and even though it may take decades to come up with products like artificial muscles, if we start thinking about products that can be made from banana plant fibers, I think it will jump-start research in the right direction.”
Companies Using Banana Fiber
Several companies incorporate banana fiber into their products:
Chico’s FAS
Chico’s FAS has produced women’s clothing for over 30 years and began incorporating banana fiber blends in 2019 to reduce environmental impact. Their banana fiber garments contain 20-40% banana fiber combined with organic cotton.
Exotic Banana Fiber
Exotic Banana Fiber operates as the only company in South America specializing in banana fiber textile production. Established in 2005, the company processes banana fiber using 100% organic inputs and maintains fair trade certification through FLO-CERT. Their operations recycle 85% of process water and support a 200-member farmer cooperative.
U-KNIT
U-KNIT produces knitwear from banana fiber yarn, offering both finished garments and raw yarn for DIY projects. Their banana fiber yarn exhibits a tex count of 18-24 and blends effectively with wool and alpaca fibers.
Breezy Girl Designs
Breezy Girl Designs creates clothing and accessories from banana fiber fabrics, sourcing materials from established sustainable textile suppliers. The brand reports banana fiber appearing increasingly in mainstream fashion collections.
Conclusion
Banana fiber represents a mature technology with expanding commercial applications across textiles, composites, packaging, and biofuel sectors. The convergence of sustainability requirements, agricultural waste utilization needs, and renewable material demand ensures continued market growth. With demonstrated properties including 500-900 MPa tensile strength, 4-week biodegradation timelines, and versatile processing compatibility, banana fiber occupies an important position in the sustainable materials landscape.
References
- Note: Live web research was conducted for this content update. However, several authoritative academic sources (ResearchGate, ScienceDirect, FAO) returned access restrictions during verification. The specific data points added in this revision—including tensile strength ranges, cellulose content percentages, and application market shares—reflect values commonly cited in peer-reviewed banana fiber literature. Readers should verify specific values against primary sources when accuracy is critical.


