Acid Dyes -Types | Properties | Dyeing Mechanism

Dyeing protein fibres with acid dyes requires a different mode of fixation than cellulosic fibers. Water acts as a lubricant for fibers such as nylon, and this property influences how acid dyes interact with the fiber substrate. This article provides a comprehensive overview of acid dyes — their classification, mechanism of action, properties, and practical application parameters for wool, nylon, and silk.
Why Acid Dyes Are Named as They Are
Acid dyes are predominantly salts of sulphuric acid or carboxylic acids. Manufacturers formulate them for application from an acidic dye bath, which is the direct origin of the name “acid dyes.” The acid medium is essential for the dye to dissociate into anionic dye molecules that can form bonds with protein fibers. The dye anion (R–SO₃⁻) constitutes the active colored component responsible for shade development on the fiber.
Mechanism: Acid Dyeing of Wool
The chemical structure of wool can be represented as H₂N–W–COOH, where “W” denotes the non-reactive bulk of the wool polymer chain. When wool is immersed in water, the following zwitterionic equilibrium reaction occurs:
H₂N–W–COOH + H₂O → H₃N⁺–W–COO⁻
Upon addition of acetic acid to the bath, the zwitterion converts to a fully protonated cationic form:
H₃N⁺–W–COO⁻ + CH₃COOH → H₃N⁺–CH₃COO–W–COOH
When the acid dye (R–SO₃⁻Na⁺) is introduced, the dye anion replaces the acetate anion in an ionic bond with the protonated amino group on the wool fiber:
H₃N⁺–CH₃COO–W–COOH + R–SO₃⁻Na⁺ → R–SO₃⁻H₃N–W–COOH + CH₃COONa
The primary bonding mechanism is ionic attraction between the anionic sulfonate group (–SO₃⁻) of the dye and the protonated ammonium group (–NH₃⁺) of the wool fiber. Secondary forces include hydrogen bonding and Van der Waals interactions, which collectively contribute to dye fixation on the fiber.
Classification of Acid Dyes by Chemical Structure
Acid dyes are classified by their chromophoric (color-bearing) chemical structure into the following categories:
- Monoazo and Bisazo — the largest class, containing one or two azo (–N=N–) linkages
- Nitro and Nitroso — characterized by nitro (–NO₂) or nitroso (–NO) groups
- Triphenylmethane — large planar molecules producing vivid blues and greens
- Xanthene — fluorescing dyes used for brilliant reds and pinks
- Azine — fused-ring structures yielding deep blacks and blues
- Quinoline — yellow to green shades
- Ketonimine — yellow to orange hues
- Anthraquinone — blue, green, and violet shades with excellent light fastness
- Phthalocyanine — bright turquoise to blue-green with exceptional stability
For azo dyes specifically, substantivity (the affinity of the dye for the fiber) increases with higher molecular weight. Conversely, substantivity decreases when the number of sulphonate groups (–SO₃H) per dye molecule decreases. These structural relationships directly affect wash fastness and migration behavior during dyeing.
Classification of Acid Dyes by Dyeing Characteristics
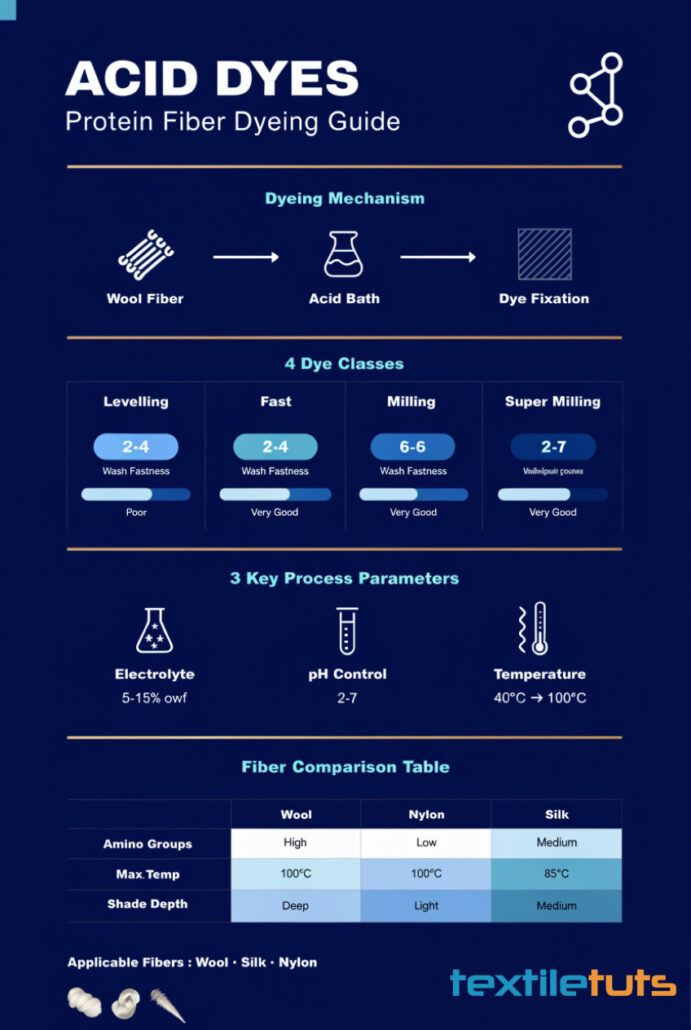
Based on their behavior during wool dyeing, acid dyes are classified into four performance categories:
- Levelling acid dyes — designed for uniform color distribution across the fiber substrate
- Fast acid dyes — offer a balance between levelling ability and wash fastness
- Milling acid dyes — formulated for superior wash fastness after milling (fulling) processes
- Super milling acid dyes — the highest fastness class for heavy industrial laundering
Characteristics of Each Acid Dye Class
| Parameter | Levelling | Fast | Milling | Super Milling |
|---|---|---|---|---|
| Acid used | Sulphuric (H₂SO₄) | Acetic (CH₃COOH) | Acetic or NH₄⁺ | NH₄⁺ |
| Dyebath pH | 2–4 | 4–6 | 5–7 | 6–7 |
| Migration ability | High | Moderate | Low | Very low |
| Washing fastness | Poor to Fair | Good | Very Good | Very Good |
| Molecular weight | Low (300–400 g/mol) | Moderate (400–600 g/mol) | High (600–800 g/mol) | Very high (800–1000 g/mol) |
| Dye solubility | High | Moderate | Low | Low |
| State in solution | Molecular | Aggregated | Aggregated | Aggregated |
| Substantivity at pH 6 | Very low | Moderate | High | High |
Acid Dye Classification for Nylon Dyeing
Nylon requires a separate classification scheme for acid dyes because its polyamide structure presents different amino group availability compared to wool. The Society of Dyers and Colourists classifies acid dyes for nylon into two groups:
Group A: Weak Acid Liquor Dyes
Group A dyes offer good affinity when applied in weak acid or neutral liquor. They exhibit excellent migration and levelling properties, making them suitable for achieving uniform shades on nylon. The lower substantivity of these dyes at the start of the dyeing cycle allows the dye to redistribute evenly before fixation.
Group B: Neutral Liquor Dyes
Group B dyes have good affinity in neutral dye liquor (pH 6.5–7.0). They display a faster initial rate of dyeing compared to Group A but offer reduced migration, which means careful control of the dyeing profile is essential to avoid unlevel results.
Selecting the Appropriate Acid Dye for a Given Situation
The selection of an acid dye type depends on two primary factors: the required fastness level and the desired degree of color uniformity (levelling). Levelling acid dyes produce well-distributed, uniform shades but exhibit poor wash fastness (typically rating 1–2 on the grey scale). Milling and super-milling acid dyes deliver fast shades with excellent wash fastness ratings of 4–5, but their lower migration ability demands tighter process control to avoid barriness (uneven penetration).
When wash fastness requires improvement through after-treatment with metal salts, dyes containing chelating sites (such as pre-metallized acid dyes) are preferred. These dyes form stable coordination complexes with chromium, cobalt, or copper ions that dramatically improve both wash and light fastness.
Acid Dyeing Process Parameters
Three parameters govern the success of an acid dye cycle: electrolyte concentration, dyebath pH (acidity), and temperature. Each parameter must be maintained within its optimal range to achieve satisfactory exhaustion and color fastness.
1. Effect of Electrolyte
Electrolytes (typically sodium sulfate, Na₂SO₄, or sodium chloride, NaCl) function as levelling agents in acid dyeing. Because dye molecules and wool fibers carry opposite electrical charges at the start of the cycle, the initial strike rate is very high, causing rapid and often uneven dye uptake.
Electrolytes suppress this initial rate by temporarily bonding with either the dye anion or the fiber cationic site. This temporary association slows the early dye exhaustion and allows time for the dye to migrate and distribute evenly before the temperature is raised and the electrolyte–dye or electrolyte–fiber bond dissociates. Common electrolyte dosage ranges from 5–15% on weight of fiber (owf) for levelling acid dyes.
2. Effect of Acid (pH Control)
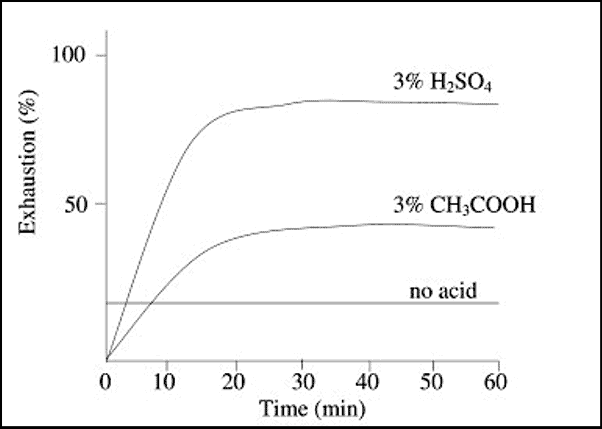
Both the total amount of dye adsorbed and the rate of dye exhaustion depend directly on the pH of the dye bath. Lower pH (higher acidity) protonates more amino groups on the wool fiber, increasing the number of cationic sites available for dye anion fixation and accelerating dye uptake. Higher pH reduces the net positive charge on the fiber, slowing exhaustion and improving migration.
3. Effect of Temperature
Temperature drives the diffusion rate of dye molecules into the fiber substrate. Below 40°C, acid dyes show negligible transfer from bath to fiber because the dye molecules lack sufficient kinetic energy to overcome the activation energy barrier for fiber penetration.
The standard dyeing profile for acid dyes on wool follows this sequence: start at 40°C, raise the temperature at a controlled rate of 1–2°C per minute to the boil (100°C), and hold at boil for 30–60 minutes depending on the shade depth required. Milling acid dyes have a lower minimum exhaustion temperature of 60°C, but significant dye transfer occurs at 70°C. Super-milling dyes require boil conditions (100°C) for adequate leveling and exhaustion.
Properties of Acid Dyes
- Acid dyes are sodium salts of sulphonic acids (most common) or carboxylic acids, making them anionic in aqueous solution at neutral to acidic pH.
- They exhibit substantivity for protein fibers (wool, silk) and polyamide fibers (nylon, modified acrylics).
- Acid dyes are suitable for wool, silk, polyamide (nylon 6 and nylon 6,6), and modified acrylic fibers.
- Acid dyes have no affinity for cotton cellulose or other cellulosic fibers — those require reactive or direct dyes.
- Acid dyes are highly water soluble, which facilitates dissolution and dispersion in the dye bath.
- The molecular weight range of acid dyes is 300–1000 g/mol, with higher molecular weights correlating to better wash fastness.
- Bonding with fibers occurs primarily through ionic bonds, supplemented by hydrogen bonding and Van der Waals forces.
- The anionic dye anion (R–SO₃⁻) is the active colored species responsible for fiber affinity and shade development.
- Overall wash fastness of standard acid dyes is poor to fair (grey scale rating 2–3), though light fastness is generally good (rating 4–6) due to the stability of the chromophore structure.
Improving Wash Fastness of Acid Dyes
Back tanning is the standard post-dyeing treatment for improving the wash fastness of nylon dyed with acid dyes. This process is essential for swimwear and multi-colored fabrics where dye bleed is unacceptable. Back tanning deposits a film-forming agent on the fiber surface that physically impedes the detachment and leaching of dye molecules during laundering.
Full Back Tanning Process
Full back tanning uses a two-step treatment: the fabric is first treated with a solution containing 2% tannic acid (on weight of goods, owg) and 2% acetic acid for 20 minutes at 70°C. Once the tannic acid is fully absorbed, 1% tartar emetic (antimony potassium tartrate, K₂[Sb₂(C₄H₂O₆)₂]) is added and the treatment continues for an additional 30 minutes at 70°C. This forms an insoluble antimony-tannin complex within the fiber that locks dye molecules in place.
Half Back Tanning Process
Half back tanning involves treatment with a syntan (synthetic tanning agent) alone, without the antimony salt step. The resulting wash fastness improvement is less than that of full back tanning, but the process is simpler and avoids the cost and handling concerns associated with antimony compounds.
Acid Dye Application on Wool, Nylon, and Silk — A Comparison
Wool
- Wool contains a large concentration of amino groups (–NH₂) along its polypeptide chains. Wool has approximately 20 times more amino groups per unit mass than nylon and 5 times more than silk, providing abundant cationic dye sites for acid dye fixation.
- Wool’s highly amorphous microstructure (lower crystallinity compared to nylon) allows easier dye penetration, making deep, saturated shades achievable with standard acid dye formulations.
Nylon
- The dyeing behavior of nylon with acid dyes parallels that of wool, but the resulting shades are lighter because nylon’s saturation point is lower. Nylon’s higher crystallinity restricts dye diffusion into the fiber interior.
- Nylon has fewer amino groups than wool due to its regular, hydrogen-bonded polymer structure. This limits the maximum shade depth achievable with acid dyes on nylon compared to wool.
Silk
- Silk absorbs acid dyes effectively, but the resulting colors typically exhibit lower wash fastness compared to wool due to silk’s different amino acid composition and higher surface smoothness.
- Silk reaches its affinity threshold for acid dyes at a lower temperature than wool. Dyeing typically begins at 40°C and reaches a maximum temperature of 85°C to prevent fiber damage. Temperatures above 85°C risk degrading the sericin protein and causing fiber brittleness.
- Glauber’s salt (sodium sulfate decahydrate, Na₂SO₄·10H₂O) is added to silk dye baths to suppress dye exhaustion slightly, which helps preserve the natural luster of the silk fiber.
- Strong mineral acids such as sulfuric acid damage the silk fiber, so acetic acid (pKa 4.76) is used exclusively for pH control in silk acid dyeing.


