
Blowroom : Function & Operations

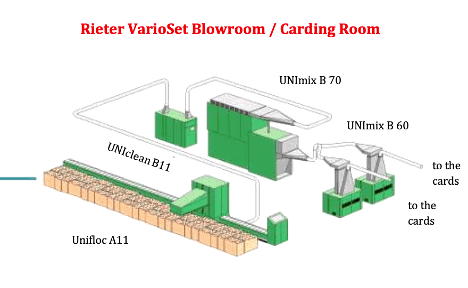
The blowroom section is the first processing unit in a textile spinning mill, where compacted cotton bales are transformed into a uniform lap suitable for carding through four sequential operations: opening, cleaning, blending, and lap formation. This process contributes approximately 10% of total ring spinning manufacturing costs, with cleaning efficiency typically ranging from 40% to 70% depending on fiber contamination levels and machine settings. The world’s leading blowroom machinery manufacturers are Rieter (Switzerland) and Trützschler (Germany).
Key Blowroom Specifications at a Glance
| Parameter | Value / Range | Notes |
|---|---|---|
| Cost Contribution | ~10% | Of total ring spinning manufacturing costs |
| Cleaning Efficiency | 40% – 70% | Depends on fiber contamination and machine settings |
| Rieter UNIfloc A 12 Throughput | Up to 2,400 kg/h | High-capacity automatic bale opener |
| Trützschler BO-P Throughput | 2,500 – 3,000 kg/h | Processes 5–7 bales simultaneously; up to 48 hr continuous operation |
| Blendomat Bale Capacity | 180 bales/laydown | Up to 48 hours continuous production |
| Tuft Size Target | ~0.1 mg per flock | Smallest possible dimension for maximum cleaning efficiency |
What is the Blowroom Section?
The blowroom is the dedicated first step in yarn manufacturing where compacted cotton bales are transformed into a uniform lap suitable for carding. This transformation occurs through four sequential operations: opening, cleaning, blending, and lap or chute formation. Each operation is carried out by specialized machines designed to progressively improve fiber quality while minimizing fiber damage.
In modern spinning mills, blowroom productivity reaches up to 2,400 kg/h on high-capacity lines such as the Rieter UNIfloc A 12. Trützschler’s Portal Bale Opener BO-P processes 2.5 to 3.0 tonnes of material per hour across 5–7 bales side by side, with uninterrupted operation lasting up to 48 hours. These throughput rates demonstrate the scale at which contemporary blowroom systems operate.
Functions of the Blowroom Section
The blowroom performs four primary functions that directly determine the quality of the final yarn:
- Opening the compacted fiber bales into individual tufts and flocks.
- Cleaning the fibers to remove dust, seed fragments, leaf matter, stems, and other contaminants.
- Blending diverse fiber categories to improve yarn quality and reduce manufacturing costs.
- Forming a uniform lap or chute feed from packed cotton bales for downstream carding.
Basic Operations in the Blowroom
The blowroom process consists of four distinct operations, each targeting a specific aspect of fiber preparation:
1. Fiber Opening
Fiber opening converts compacted bales into small, manageable flocks. The objective is to reduce tuft size to the smallest possible dimension. Each flock or tuft is condensed to approximately 0.1 mg, which allows subsequent cleaning elements to operate with maximum efficiency.
2. Fiber Cleaning
Contaminants including dust, fragmented seeds, dry leaves, stems, and external foreign matter are eliminated from the fiber mass. Cleaning efficiency is measured by the Cleaning Index CT = (DF − DD) / DF × 100%, where DF represents dirt in the feed material and DD represents dirt in the delivered material.
3. Fiber Mixing or Blending
Fibers of the same or different grades are thoroughly mixed and blended to produce consistent yarn quality while reducing raw material costs. Homogeneous blending ensures that each length of spun yarn contains a uniform proportion of each fiber component.
4. Lap or Chute Formation
Opened and cleaned flocks are formed into a thin, uniform sheet called a lap. The lap has a controlled width and a predetermined length per unit weight. Modern blowroom lines use the chute feed system, which delivers fiber directly to the card in a controlled, even stream without requiring manual lap handling.
Weight consistency of laps from the scutcher determines the uniformity of material fed to the carding machine. Even lap weight distribution directly impacts yarn quality downstream in the spinning process.
Operating Zones in the Blowroom
| Operating Zone | Function | Typical Machines |
|---|---|---|
| 01. Gradual Opening | Opening bales progressively into small tufts. | Automatic Bale Opener; Unifloc (Rieter); Blendomat (Trützschler). |
| 02. Extensive Cleaning | Removing trash particles larger than 500 µm. | Step Cleaner; Uniclean (Rieter). |
| 03. Blending or Mixing | Homogeneous mixing of fiber types and grades. | Integrated Multimixer (Trützschler); Unimix (Rieter). |
| 04. Fine Cleaning | Eliminating macro-dust in the 50–500 µm range. | RN Cleaner (Trützschler); Uniflex (Rieter). |
| 05. Intensive Cleaning | Removing micro-dust in the 15–50 µm range. | ERN Cleaner (Rieter); Kirschner Beater. |
| 06. Lap or Chute Feed | Delivering uniform feed to the carding machine. | Lap Feed; Chute Feed A11 (Rieter). |
Fiber Opening Processes
Fibers are opened progressively, forming small tufts or flocks that reach the card as either a lap or via chute feed. In the card and open-end spinning systems, opening continues until each fiber is fully individualized. Two distinct stages of opening occur across the blowroom and carding department.
- Opening the flocks within the blowroom section.
- Opening the fibers within the card and open-end spinning frames.
Factors That Determine Opening and Cleaning Quality
The accuracy of fiber opening and the intensity of cleaning, along with the risk of fiber damage, are influenced by the following parameters:
- Design and type of the opening device.
- Rotational speed (RPM) of the opening device.
- Depth of penetration through the fiber mass.
- Form and method of feed introduction.
- Distance between the feed material and the opening device.
- Grid bar design and configuration.
- Total surface area of the grid.
- Airflow settings within the grid chamber.
- Condition and degree of pre-opening applied.
- Width of the input fiber web.
- Material delivery rate through the machine.
- Positioning and arrangement of the device within the machine series.
Opening Devices Used in the Blowroom
| Device Type | Appearance | Description |
|---|---|---|
|
Rollers | 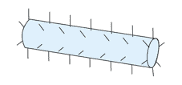 | Small diameter rollers widely used in step cleaners for targeted opening action. |
|
Drums | 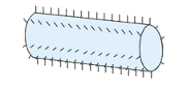 | Large diameter drums used in the mono-cylinder cleaner for high-capacity processing. |
|
Quilted Shaft | 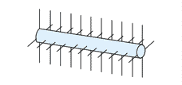 | Shaft equipped with multiple long beater rods; rarely used in modern installations. |
|
Multiple-Blade Beater | 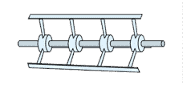 | Two, three, or more armed configurations; now found only in older blowroom lines. |
|
Spiked Lattice | 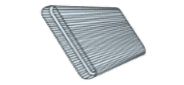 | Endless belts fitted with transverse wooden or plastic bars holding needles; provides very gentle fiber opening. |
|
Picker | 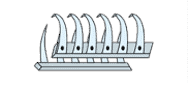 | Used in bale pickers and blending grabs; now considered outdated technology. |
|
Carding Bars or Plates | 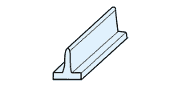 | Components associated with the carding drums of the carding machine. |
Fiber Cleaning in the Blowroom
Contaminant removal directly determines the ultimate quality of spun yarn. Higher cleaning efficiency improves yarn strength, reduces breakage during spinning, and produces a smoother final product. The Cleaning Index CT provides a quantitative measure of cleaning performance.
Cleaning Index CT = (DF − DD) / DF × 100%
Where DF is the dirt content in the feed material and DD is the dirt content in the delivered material after cleaning. Blowroom cleaning efficiency typically falls between 40% and 70%, with the upper limit imposed by fiber damage risks at higher beater speeds.
Key Machine Components of the Blowroom
Grid Bars and Elements
Grids are horizontal trough-shaped devices composed of multiple individual multilateral bars or blades that together form a rack beneath the opening segment. Grid elements include perforated and slotted sheets, triangular segmented bars, angular bars, and multilateral blades. The precise arrangement of these elements controls airflow and fiber trajectory during cleaning.
Major Blowroom System Configurations
Trützschler Blowroom Line
Automatic Bale Opener Blendomat BO-A
↓
Multi-Function Separator SP-MF
↓
Multimixer
↓
Clenomat Cleaner
↓
Foreign Part Separator
↓
De-dustex
↓
Chute Feed
Unifloc A 12
↓
Uniclean B 12
↓
Unimix B 12
↓
Uniflex / Unistore
↓
Chute Feed A11
Trützschler Blowroom Line
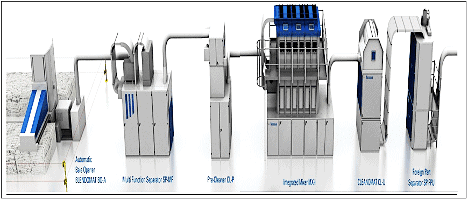
Blendomat BDT Bale Opener Specifications
- Provides gentle, gradual, and uniform fiber opening from compressed bales.
- Maximum productivity reaches 1,500 kg/hr under standard operating conditions.
- Simple machine operation with straightforward operator controls.
- Minimal maintenance requirements reduce unplanned downtime.
- Wide application range across multiple cotton fiber types.
- Processes up to 3 groups of bales simultaneously during a single laydown.
- Handles 180 bales per laydown with continuous production running for 48 hours.
- Supports both lot-based and constant bale supply operating modes.
- Integrated process visualization interface for real-time monitoring.
Multi-Function Separator SP-MF Specifications
The Multi-Function Separator SP-MF is positioned downstream of the Automatic Bale Opener BO-A. All operational functions run continuously. The manufacturing rate reaches up to 2,000 kg/hr, governed by an integrated microcomputer control system.
- Operates using the suction pressure system sourced from the BLENDOMAT unit.
- Provides heavy-duty cleaning of coarse contaminants from the fiber stream.
- Detects and separates metallic foreign parts from the fiber mass.
- Eliminates dust particles from the fiber before further processing.
- Feeds waste material directly to the waste collection system.
Multimixer Specifications
The Trützschler Multimixer delivers dedicated solutions for single-component staple fiber mixing. The system achieves superior yarn quality through precise and reproducible blending across all fiber constituents.
- Dedicated mixer configurations are available for every mixing task requirement.
- Maximum homogeneity is achieved through precise and reproducible blending operations.
- Uniform product appearance results from consistent mixing quality across batches.
Clenomat Cleaner Specifications
The Clenomat delivers finest fiber opening and cleaning simultaneously with exceptionally smooth fiber handling at throughput rates of 1,000 kg/hr and above.
- Cleaning intensity is easily adjustable via modifiable cleaning elements, even during active production.
- Optimal adaptation to individual cotton varieties uses specifically engineered wire and saw-tooth rollers.
- Rapid raw material changeovers occur through highly adjustable roll drive settings.
- Direct suction keeps the machine clean and allows processing of humid fibers.
- Superior yarn quality and enhanced running performance in open-end and ring spinning result from stable dust cleaning.
- Maintenance-free electric motors and belt drives eliminate ongoing maintenance expenses.
- Integrated Trützschler microcomputers provide stable monitoring and accuracy control.
Foreign Part Separator Specifications
- Delivers state-of-the-art separation technology for foreign object detection.
- Incorporates diversified detection units and advanced lighting technology for thorough inspection.
- Detects opaque, colorless, and white polypropylene (PP) contamination that standard systems miss.
- Identifies transparent, semi-transparent, and fluorescent foreign matter in the fiber stream.
- Integrated high-performance dust detection module makes this system suitable for rotor spinning mills.
De-dustex Specifications
- Provides high-accuracy dust separation at the end of the blowroom cleaning line.
- Efficiently removes even micro-sized dust particles from the fiber stream.
- Particularly suitable for open-end and air-jet yarn manufacturing applications.
Rieter Blowroom Line
UNIfloc A 12 Specifications
The UNIfloc A 12 is Rieter’s flagship automatic bale opener. It collects fibers uniformly from all bales in a laydown, opens them gradually and gently into the smallest possible flocks, and initiates blending from the very start of the process. The system operates at line production rates of up to 2,400 kg/h.
- Collects fibers uniformly from every bale in a simultaneous laydown configuration.
- Opens fibers gradually and gently to minimize fiber damage and preserve quality.
- Reduces tufts to the smallest possible flock size for maximum cleaning efficiency.
- Produces flocks of uniform size across all processed bales.
- Processes the maximum possible number of bales per production cycle in a single up-and-down movement.
- Universally applicable design with straightforward operation and maintenance.
- Begins fiber blending immediately at the start of the process sequence.
- Enables blending of fiber from multiple origins and constituents in a single pass.
Uniclean B 12 Specifications
The Uniclean B 12 delivers superior fiber cleaning through free fiber movement and adaptable grid bars. The system operates at delivery speeds of up to 1,400 kg/hr of card sliver with effective fiber realization exceeding conventional cleaners by up to 2%.
- Achieves superior cleaning through free fiber movement combined with adaptable grid bars.
- Extended dust removal surface ensures thorough cleaning even at elevated production rates.
- Simple visual inspection enables rapid assessment of waste quality and composition.
- Designed for delivery speeds of up to 1,400 kg/hr of card sliver.
- Fiber realization rates reach up to 2% higher than conventional cleaning systems.
- Alternating extraction reduces energy consumption for waste transportation.
- VARIOset technology automatically designates the operating format specific to each fiber variety.
- Connects to the Unicontrol blowroom control system for integrated process management.
UNImix B 12 and B 76 Specifications
The UNImix system provides uniform blending of fibers at delivery speeds reaching 800 kg/h. The eight-chamber blending configuration delivers an extended storage capacity and exceptional flexibility across diverse fiber materials.
- Delivers uniform fiber blending across all material types and fiber grades.
- Achieves high throughput rates with delivery speeds reaching 800 kg/h.
- Simple mechanical arrangement minimizes complexity and maintenance requirements.
- Few wearing parts reduce ongoing operational costs and downtime.
- Eight-chamber blending configuration ensures thorough mixing of all fiber constituents.
- Extended storage capacity provides greater flexibility during material changeovers.
- Exceptional flexibility accommodates diverse fiber materials across multiple product lines.
Uniflex and Unistore Specifications
The Uniflex and Unistore units provide fine cleaning of blended cotton fiber. The RPM of the beater, the number of spikes, and the grid bar settings all critically determine the cleaning effectiveness achieved on the cotton.
- Serves as the fine cleaning stage within the Rieter blowroom sequence.
- Receives blended cotton and performs thorough contamination removal.
- Reduces cotton tufts to very small dimensions while eliminating leaf matter, sand, and similar contaminants without fiber damage.
- Beater RPM, spike count, and grid bar configuration all critically determine cleaning effectiveness.
Chute Feed System vs Lap Feed System
The chute feed system delivers fiber to the carding machine as small tufts or flocks rather than as a pre-formed lap. Carding machines process these fiber tufts more effectively than traditional lap sheets. The chute feed system reduces the manpower required for lap handling and achieves higher production rates on modern carding lines. Continuous chute feeding provides more consistent fiber distribution to each carding point compared to intermittent lap feeding.
Why the Blowroom is Separated from Carding and Spinning
Cotton bales contain significant quantities of contaminants including dust, trash, and organic impurities. Cleaning is the primary function of the blowroom, and this section operates under consistently high contamination levels. The blowroom is physically separated from downstream carding and spinning areas to prevent recontamination of cleaned fibers. Fiber that has undergone multiple cleaning passes in the blowroom must not contact unprocessed waste or dusty air streams from the bale opening area.
Why Complete Cleaning Is Not Performed in the Blowroom
Two primary factors prevent 100% cleaning of fiber in the blowroom. First, higher cleaning intensity generates greater waste volume, which directly reduces the mill’s fiber yield and erodes profitability. Spinning mills maintain typical cleaning efficiency between 40% and 70% as an optimal balance between fiber cleanliness and economic viability. Second, aggressive cleaning at elevated beater speeds causes increased fiber breakage and damage, which compromises yarn strength and spinning performance. Mills set blowroom cleaning to approximately 70% efficiency as a standard practice that preserves fiber quality while maximizing commercial return.


