
Bale Management in Spinning: Blending | Mixing

- Confers specific visual and tactile properties to end products such as PC (polyester-cotton) and CVC (chief-value cotton) fabrics with defined blend ratios.
- Offsets natural differences between cotton lots by combining bales from multiple origins to achieve consistent fiber平均值 across the blend.
- Lowers raw material cost by 8–12% through strategic substitution of expensive long-staple cotton with shorter-staple varieties that meet end-product requirements when blended correctly.
- Improves processing performance by reducing carded yarn end breaks to 30–50 per 100,000 spindle hours and combed yarn to fewer than 15 per 100,000 spindle hours.
- Produces fancy yarns such as mélangé yarn by intentionally blending fibers with different dye affinities to create color effects through differential absorption.
Types of Blending Operations and Process Stages
Blending occurs at multiple stages of the spinning process, each offering distinct advantages for specific yarn types and quality targets:
| Blending Type | Process Stage | Typical Application |
|---|---|---|
| 01. Bale blending | Before the blow room | Open-end and ring-spun coarse counts (Ne 4–20) |
| 02. Flock blending | Within the blow room | Carded medium counts (Ne 10–40) |
| 03. Lap blending | Using doubling scutcher | Carded fine counts (Ne 30–60) |
| 04. Web blending | At the ribbon lap machine | Combed yarns requiring high uniformity |
| 05. Sliver blending | At the draw frame and comber | Combed and compact yarns (Ne 30–120) |
| 06. Fiber blending | At the carding machine | Blended hosiery and weaving yarns |
| 07. Roving blending | At the ring spinning machine | Specialty and novelty yarns only |
Difference Between Mixing and Blending
| Mixing | Sl. | Blending |
|---|---|---|
| Combines fibers in non-proportioned, stochastic ratios. | 01 | Combines fibers in precisely calculated, documented proportions. |
| Resulting yarn properties cannot be reliably predicted before spinning. | 02 | Resulting yarn properties are predictable within ±1% of target values. |
| Difficult to reproduce across different lots or orders. | 03 | Easily reproduced by reapplying the same proportion formula. |
Frequently Asked Questions
Selecting Bales for Laydown Using SCI Data
When multiple test results create complexity in selecting appropriate bales for a laydown, the Spinning Consistency Index (SCI) provides a single derived value that summarizes fiber spinnability. Fibers with an SCI value below 120 are unsuitable for fine spinning—the minimum threshold for ring frame processing of Ne 30 and above. The SCI formula integrates fiber strength, micronaire, length, uniformity, and color into one predictive score:
Spinning Consistency Index (SCI) = -414.67 + 2.9 × Strength (cN/tex) − 9.32 × Micronaire + 49.17 × Length (inches) + 4.74 × Uniformity Index (%) + 0.65 × Rd + 0.36 × +b
HVI systems automatically calculate SCI for each tested bale. Mills should maintain no more than 5–7 SCI categories in a blend to control processing consistency while utilizing the full warehouse inventory.
Achieving Consistent Yarn Quality Through Bale Management
Producing 100% consistent yarn quality is not achievable in practice. Fiber diameter (micronaire) varies by ±0.3 units even within a single bale, and fiber length distribution shows coefficient of variation (CV) of 35–45% for upland cottons. These inherent material variations, combined with mechanical processing inconsistencies in carding (nep generation: 50–100 per gram) and ring spinning (yarn tension CV: 8–15%), preclude absolute consistency. However, well-executed bale management reduces yarn quality variation to ±2% of target values—well within buyer specifications for commercial textile production.
Blending vs. Mixing: Why Blending is Preferred for Commercial Spinning
Blending is the standard method for commercial spinning because it maintains consistent fiber proportions that can be replicated across successive production lots. Mixing introduces uncontrolled variability because the fiber ratio is not held constant, causing yarn quality to shift from lot to lot and order to order. Since yarn buyers enforce strict tolerance bands on count (CV ≤ 1.5%), strength (CV ≤ 3.0%), and evenness (CV ≤ 2.0%), blending’s reproducibility is essential for sustaining commercial viability. Mills that rely on mixing require 15–25% more fiber testing and re-verification, increasing laboratory costs by an estimated 20% compared to blending-based production.
Spinning Fibers to Yarn at Small Scale
Small-scale and hobby spinners use spinning wheels such as the Ashford Kiwi 3, Ashford Traditional, or Lendrum upright wheel to convert fiber into yarn. These machines produce singles yarn at 80–200 meters per hour depending on wheel diameter (65–90 cm) and spindle type. While production rates are not comparable to industrial ring frames (producing 20–50 kg per spindle per hour), spinning wheels enable precise control over twist (TPI 4–12 for wool, 8–20 for cotton) and are suitable for producing 50–200 grams of yarn per session for hand-knitting, crochet, and craft applications.
Yarn Count Impact on Bale Blending and Mixing in Spinning
Yarn count is a critical parameter that determines fiber selection during bale blending and mixing in spinning. Different yarn count systems—including English count (Ne), metric count (Nm), and tex—require specific fiber property ranges to achieve the desired yarn characteristics. With yarn count systems explained, spinners align fiber properties such as strength (cN/tex), length (mm), and fineness (mTex) with the target yarn count to ensure processing efficiency and final yarn quality. Coarse counts (Ne 4–20) tolerate shorter fibers (19–25 mm) and lower strength (18–25 cN/tex), while fine counts (Ne 40–120) require long fibers (28–36 mm) and high strength (30–45 cN/tex).
References
- ASTM International. (2021). ASTM D1776/D1776M-21: Standard Practice for Conditioning and Testing Textiles. ASTM International.
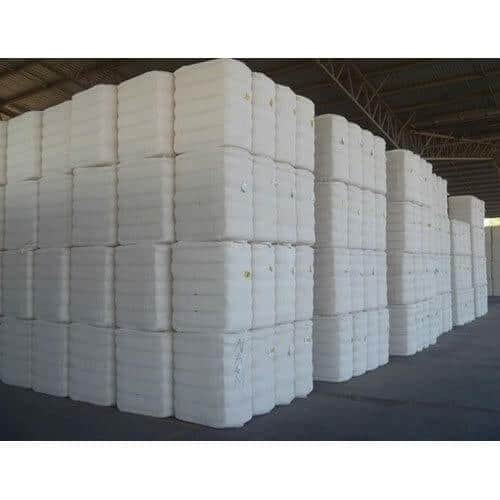
Bale management is the process of selecting, categorizing, and homogeneously blending cotton bales according to fiber characteristics to produce yarn with consistent quality at minimum raw material cost. Spinning facilities use fiber testing data, mixing optimization, and production planning to ensure repeatable spinning performance across every batch.
The discipline integrates HVI (High Volume Instrument) and AFIS (Advanced Fiber Information System) test results into a Bale Inventory and Analysis System (BIAS), then applies regression analysis or linear programming to generate an optimized blending plan before executing the laydown in the blowroom.
Key Bale Management Parameters at a Glance
Use this quick-reference table to match fiber properties to your target yarn count. These ranges represent acceptable values for commercial spinning operations:
| Parameter | Coarse Counts (Ne 4–20) | Medium Counts (Ne 10–40) | Fine Counts (Ne 40–120) |
|---|---|---|---|
| Fiber Length (mm) | 19–25 | 24–28 | 28–36 |
| Fiber Strength (cN/tex) | 18–25 | 24–30 | 30–45 |
| Micronaire | 3.5–5.0 | 3.0–4.5 | 2.5–4.0 |
| Uniformity Index (%) | ≥ 76 | ≥ 80 | ≥ 83 |
| Short Fiber Content (%) | ≤ 18 | ≤ 14 | ≤ 10 |
| Nep Count (per gram) | ≤ 250 | ≤ 180 | ≤ 150 |
| SCI Minimum | 100 | 110 | 120 |
Why Bale Management is Necessary
Effective bale management delivers measurable advantages throughout the spinning process:
- Ensures consistent yarn quality across batches by controlling fiber property variation to within ±5% of target values.
- Achieves required yarn specifications including strength (18–45 cN/tex depending on count), evenness (U% ≤ 12.5%), and nep count (≤ 150 per gram for combed yarn).
- Reduces shade deviation in dyed fabrics to ΔE < 1.0 CIELAB units, meeting industrial tolerance standards.
- Compensates for natural variation in raw cotton fiber properties including strength (18.5–43.0 cN/tex), length (19–36 mm), and micronaire (2.5–6.0).
- Minimizes fabric barre defects, which cost textile mills an estimated 2–5% of fabric sales value when uncontrolled.
- Delivers specific end-product quality attributes including yarn count (Ne 8–120), twist multiplier (3.5–5.0), and hairiness index (H ≤ 5.0).
- Reduces raw material expenditure by 8–15% through optimized blending that avoids over-specification of expensive fiber grades.
How Bale Management Minimizes Cost
The following mechanisms deliver measurable cost savings:
- Essential fiber properties combined with a precisely calculated blend enable use of economical raw materials that still meet all yarn specifications. Maintaining fiber property variation within ±3% of target values across a blend reduces waste fiber by 4–7%.
- Correct raw material selection paired with controlled spinning conditions reduces end breaks to fewer than 20 per 100,000 spindle hours on ring frames, enabling processing speeds of 12,000–18,000 rpm and lowering manufacturing cost per kilogram of yarn by 6–12%.
Process Sequences of Bale Management
The standard bale management workflow follows these sequential steps:
- Collect fiber samples from all cotton bales using a classer or automated sampling system—typically 150–200 grams per bale.
- Assign a unique identification number to each bale and log it in the Bale Inventory and Analysis System (BIAS) or mill ERP system.
- Condition samples at standard moisture regain (M.R.) of 8.5% for cotton for 24 hours at 20°C (±2°C) and 65% relative humidity (±2%) per ASTM D1776.
- Test each sample using HVI (High Volume Instrument) for fiber length, strength, uniformity, micronaire, color, and trash; and AFIS (Advanced Fiber Information System) for nep count, short fiber content, and fineness.
- Enter all HVI and AFIS data into BIAS (Bale Inventory and Analysis System) for statistical analysis and blend optimization.
- If BIAS is unavailable, use Microsoft Excel with statistical functions or manual calculation to analyze HVI results against target specifications.
- Generate the mixing and blending plan using regression analysis or linear programming to minimize cost while meeting yarn quality targets.
- Execute the laydown plan by arranging bales in the prescribed spatial sequence for uniform feeding into the blowroom.
HVI and AFIS Test Results for Two Different Bale Lots
The table below compares fiber properties from two cotton origins as measured by HVI and AFIS instruments. These values illustrate how bale management categorizes and separates fiber lots for appropriate end-use matching.
| Test Parameter | Cotton: Burkina Faso – 1110 | Cotton: Mali – 1320 |
|---|---|---|
| UHML (mm) | 27.01 | 27.02 |
| ML (mm) | 21.67 | 21.86 |
| UI (%) | 80.3 | 80.9 |
| Elongation (%) | 6.6 | 6.5 |
| Strength (cN/tex) | 29.6 | 29.2 |
| Micronaire | 4.13 | 3.93 |
| Moisture Regain (%) | 0.87 | 0.86 |
| Rd (Reflectance) | 77.0 | 73.8 |
| +b (Yellowness) | 11.2 | 10.3 |
| Color Grade | Good Middling | Strict Middling |
| SFI (%) | 11.3 | 10.6 |
| RiSI (Index) | 122.3 | 124.1 |
| Neps (Cnt/g) | 239 | 321 |
| Neps (μm) | 716 | 702 |
| SCN (Cnt/g) | 10 | 7 |
| SCN (μm) | 1392 | 1172 |
| L(w) mm | 22.5 | 22.6 |
| L(w) % CV | 37.5 | 39.5 |
| SFC(w) % <12.7 mm | 12.0 | 12.8 |
| UQL(w) mm | 28.1 | 28.3 |
| L(n) mm | 17.1 | 16.7 |
| L(n) % CV | 56.1 | 59.5 |
| SFC(n) % <12.7 mm | 33.3 | 36.0 |
| 5.0% Span Length (mm) | 32.1 | 32.4 |
| Fine (mTex) | 144 | 137 |
| IFC (%) | 19.6 | 20.3 |
| Maturation Ratio | 0.80 | 0.79 |
Bale Mixing
Mixing is the process of combining fibers in non-proportioned quantities so that the resulting blend characteristics cannot be reliably predicted or reproduced in subsequent batches. This stochastic approach introduces controlled variability for specific end products where slight property fluctuations are acceptable or desirable.
Minimizing Mixing Cost Through Proportion Optimization
The following example demonstrates how proportion optimization reduces fiber cost per kilogram of yarn:
When three cotton lots priced at Tk. 60.00, Tk. 70.00, and Tk. 80.00 per kilogram are combined in a proportion of 25:25:50, the weighted average cost calculates as:
Average mixing cost = [(25 × 60) + (25 × 70) + (50 × 80)] ÷ 100 = Tk. 72.50/kg
Using only the premium cotton at Tk. 80.00/kg increases raw material cost by 10.3%. Using only the economy grades at Tk. 60.00–70.00/kg fails to meet buyer specifications for yarn strength (minimum 28 cN/tex) and uniformity (U% ≤ 13.0%). The optimized 25:25:50 blend satisfies all quality requirements at Tk. 72.50/kg—a savings of Tk. 7.50/kg (9.4%) compared to the all-premium alternative while maintaining all specified yarn properties.
Bale Blending
Blending is the process of combining different cotton varieties or grades in precisely calculated proportions so that the resulting fiber blend delivers predictable, reproducible yarn quality. Unlike mixing, blending maintains known ratios of each fiber component, enabling tight control over final yarn properties within ±1% of target values.
Importance of Blending in Spinning Operations
- Confers specific visual and tactile properties to end products such as PC (polyester-cotton) and CVC (chief-value cotton) fabrics with defined blend ratios.
- Offsets natural differences between cotton lots by combining bales from multiple origins to achieve consistent fiber平均值 across the blend.
- Lowers raw material cost by 8–12% through strategic substitution of expensive long-staple cotton with shorter-staple varieties that meet end-product requirements when blended correctly.
- Improves processing performance by reducing carded yarn end breaks to 30–50 per 100,000 spindle hours and combed yarn to fewer than 15 per 100,000 spindle hours.
- Produces fancy yarns such as mélangé yarn by intentionally blending fibers with different dye affinities to create color effects through differential absorption.
Types of Blending Operations and Process Stages
Blending occurs at multiple stages of the spinning process, each offering distinct advantages for specific yarn types and quality targets:
| Blending Type | Process Stage | Typical Application |
|---|---|---|
| 01. Bale blending | Before the blow room | Open-end and ring-spun coarse counts (Ne 4–20) |
| 02. Flock blending | Within the blow room | Carded medium counts (Ne 10–40) |
| 03. Lap blending | Using doubling scutcher | Carded fine counts (Ne 30–60) |
| 04. Web blending | At the ribbon lap machine | Combed yarns requiring high uniformity |
| 05. Sliver blending | At the draw frame and comber | Combed and compact yarns (Ne 30–120) |
| 06. Fiber blending | At the carding machine | Blended hosiery and weaving yarns |
| 07. Roving blending | At the ring spinning machine | Specialty and novelty yarns only |
Difference Between Mixing and Blending
| Mixing | Sl. | Blending |
|---|---|---|
| Combines fibers in non-proportioned, stochastic ratios. | 01 | Combines fibers in precisely calculated, documented proportions. |
| Resulting yarn properties cannot be reliably predicted before spinning. | 02 | Resulting yarn properties are predictable within ±1% of target values. |
| Difficult to reproduce across different lots or orders. | 03 | Easily reproduced by reapplying the same proportion formula. |
Frequently Asked Questions
Selecting Bales for Laydown Using SCI Data
When multiple test results create complexity in selecting appropriate bales for a laydown, the Spinning Consistency Index (SCI) provides a single derived value that summarizes fiber spinnability. Fibers with an SCI value below 120 are unsuitable for fine spinning—the minimum threshold for ring frame processing of Ne 30 and above. The SCI formula integrates fiber strength, micronaire, length, uniformity, and color into one predictive score:
Spinning Consistency Index (SCI) = -414.67 + 2.9 × Strength (cN/tex) − 9.32 × Micronaire + 49.17 × Length (inches) + 4.74 × Uniformity Index (%) + 0.65 × Rd + 0.36 × +b
HVI systems automatically calculate SCI for each tested bale. Mills should maintain no more than 5–7 SCI categories in a blend to control processing consistency while utilizing the full warehouse inventory.
Achieving Consistent Yarn Quality Through Bale Management
Producing 100% consistent yarn quality is not achievable in practice. Fiber diameter (micronaire) varies by ±0.3 units even within a single bale, and fiber length distribution shows coefficient of variation (CV) of 35–45% for upland cottons. These inherent material variations, combined with mechanical processing inconsistencies in carding (nep generation: 50–100 per gram) and ring spinning (yarn tension CV: 8–15%), preclude absolute consistency. However, well-executed bale management reduces yarn quality variation to ±2% of target values—well within buyer specifications for commercial textile production.
Blending vs. Mixing: Why Blending is Preferred for Commercial Spinning
Blending is the standard method for commercial spinning because it maintains consistent fiber proportions that can be replicated across successive production lots. Mixing introduces uncontrolled variability because the fiber ratio is not held constant, causing yarn quality to shift from lot to lot and order to order. Since yarn buyers enforce strict tolerance bands on count (CV ≤ 1.5%), strength (CV ≤ 3.0%), and evenness (CV ≤ 2.0%), blending’s reproducibility is essential for sustaining commercial viability. Mills that rely on mixing require 15–25% more fiber testing and re-verification, increasing laboratory costs by an estimated 20% compared to blending-based production.
Spinning Fibers to Yarn at Small Scale
Small-scale and hobby spinners use spinning wheels such as the Ashford Kiwi 3, Ashford Traditional, or Lendrum upright wheel to convert fiber into yarn. These machines produce singles yarn at 80–200 meters per hour depending on wheel diameter (65–90 cm) and spindle type. While production rates are not comparable to industrial ring frames (producing 20–50 kg per spindle per hour), spinning wheels enable precise control over twist (TPI 4–12 for wool, 8–20 for cotton) and are suitable for producing 50–200 grams of yarn per session for hand-knitting, crochet, and craft applications.
Yarn Count Impact on Bale Blending and Mixing in Spinning
Yarn count is a critical parameter that determines fiber selection during bale blending and mixing in spinning. Different yarn count systems—including English count (Ne), metric count (Nm), and tex—require specific fiber property ranges to achieve the desired yarn characteristics. With yarn count systems explained, spinners align fiber properties such as strength (cN/tex), length (mm), and fineness (mTex) with the target yarn count to ensure processing efficiency and final yarn quality. Coarse counts (Ne 4–20) tolerate shorter fibers (19–25 mm) and lower strength (18–25 cN/tex), while fine counts (Ne 40–120) require long fibers (28–36 mm) and high strength (30–45 cN/tex).
References
- ASTM International. (2021). ASTM D1776/D1776M-21: Standard Practice for Conditioning and Testing Textiles. ASTM International.


